High-grade metal pipe weld efficiency
Optimizing Weld Seam Performance in High-Strength Pipeline Steels: Enhancing Fracture Toughness as a result of Weld Material Formulation and Heat Input Control
Introduction to High-Strength Pipeline Steels and Welding Challenges
High-energy pipeline steels, categorised underneath API 5L requirements along with X80 (minimal yield capability of 80 ksi or 555 MPa) and better grades like X100 (690 MPa), are severe for contemporary vigor infrastructure, allowing the transport of oil and gas over lengthy distances with lowered material usage and better efficiency. These steels are regularly top-power low-alloy (HSLA) compositions, microalloyed with supplies like niobium (Nb), titanium (Ti), and boron (B) to reap most beneficial energy-to-weight ratios and resistance to deformation beneath top-power situations. However, welding those substances supplies crucial challenges resulting from their susceptibility to microstructural differences during the welding procedure, which will compromise the integrity of the weld seam and heat-affected region (HAZ).
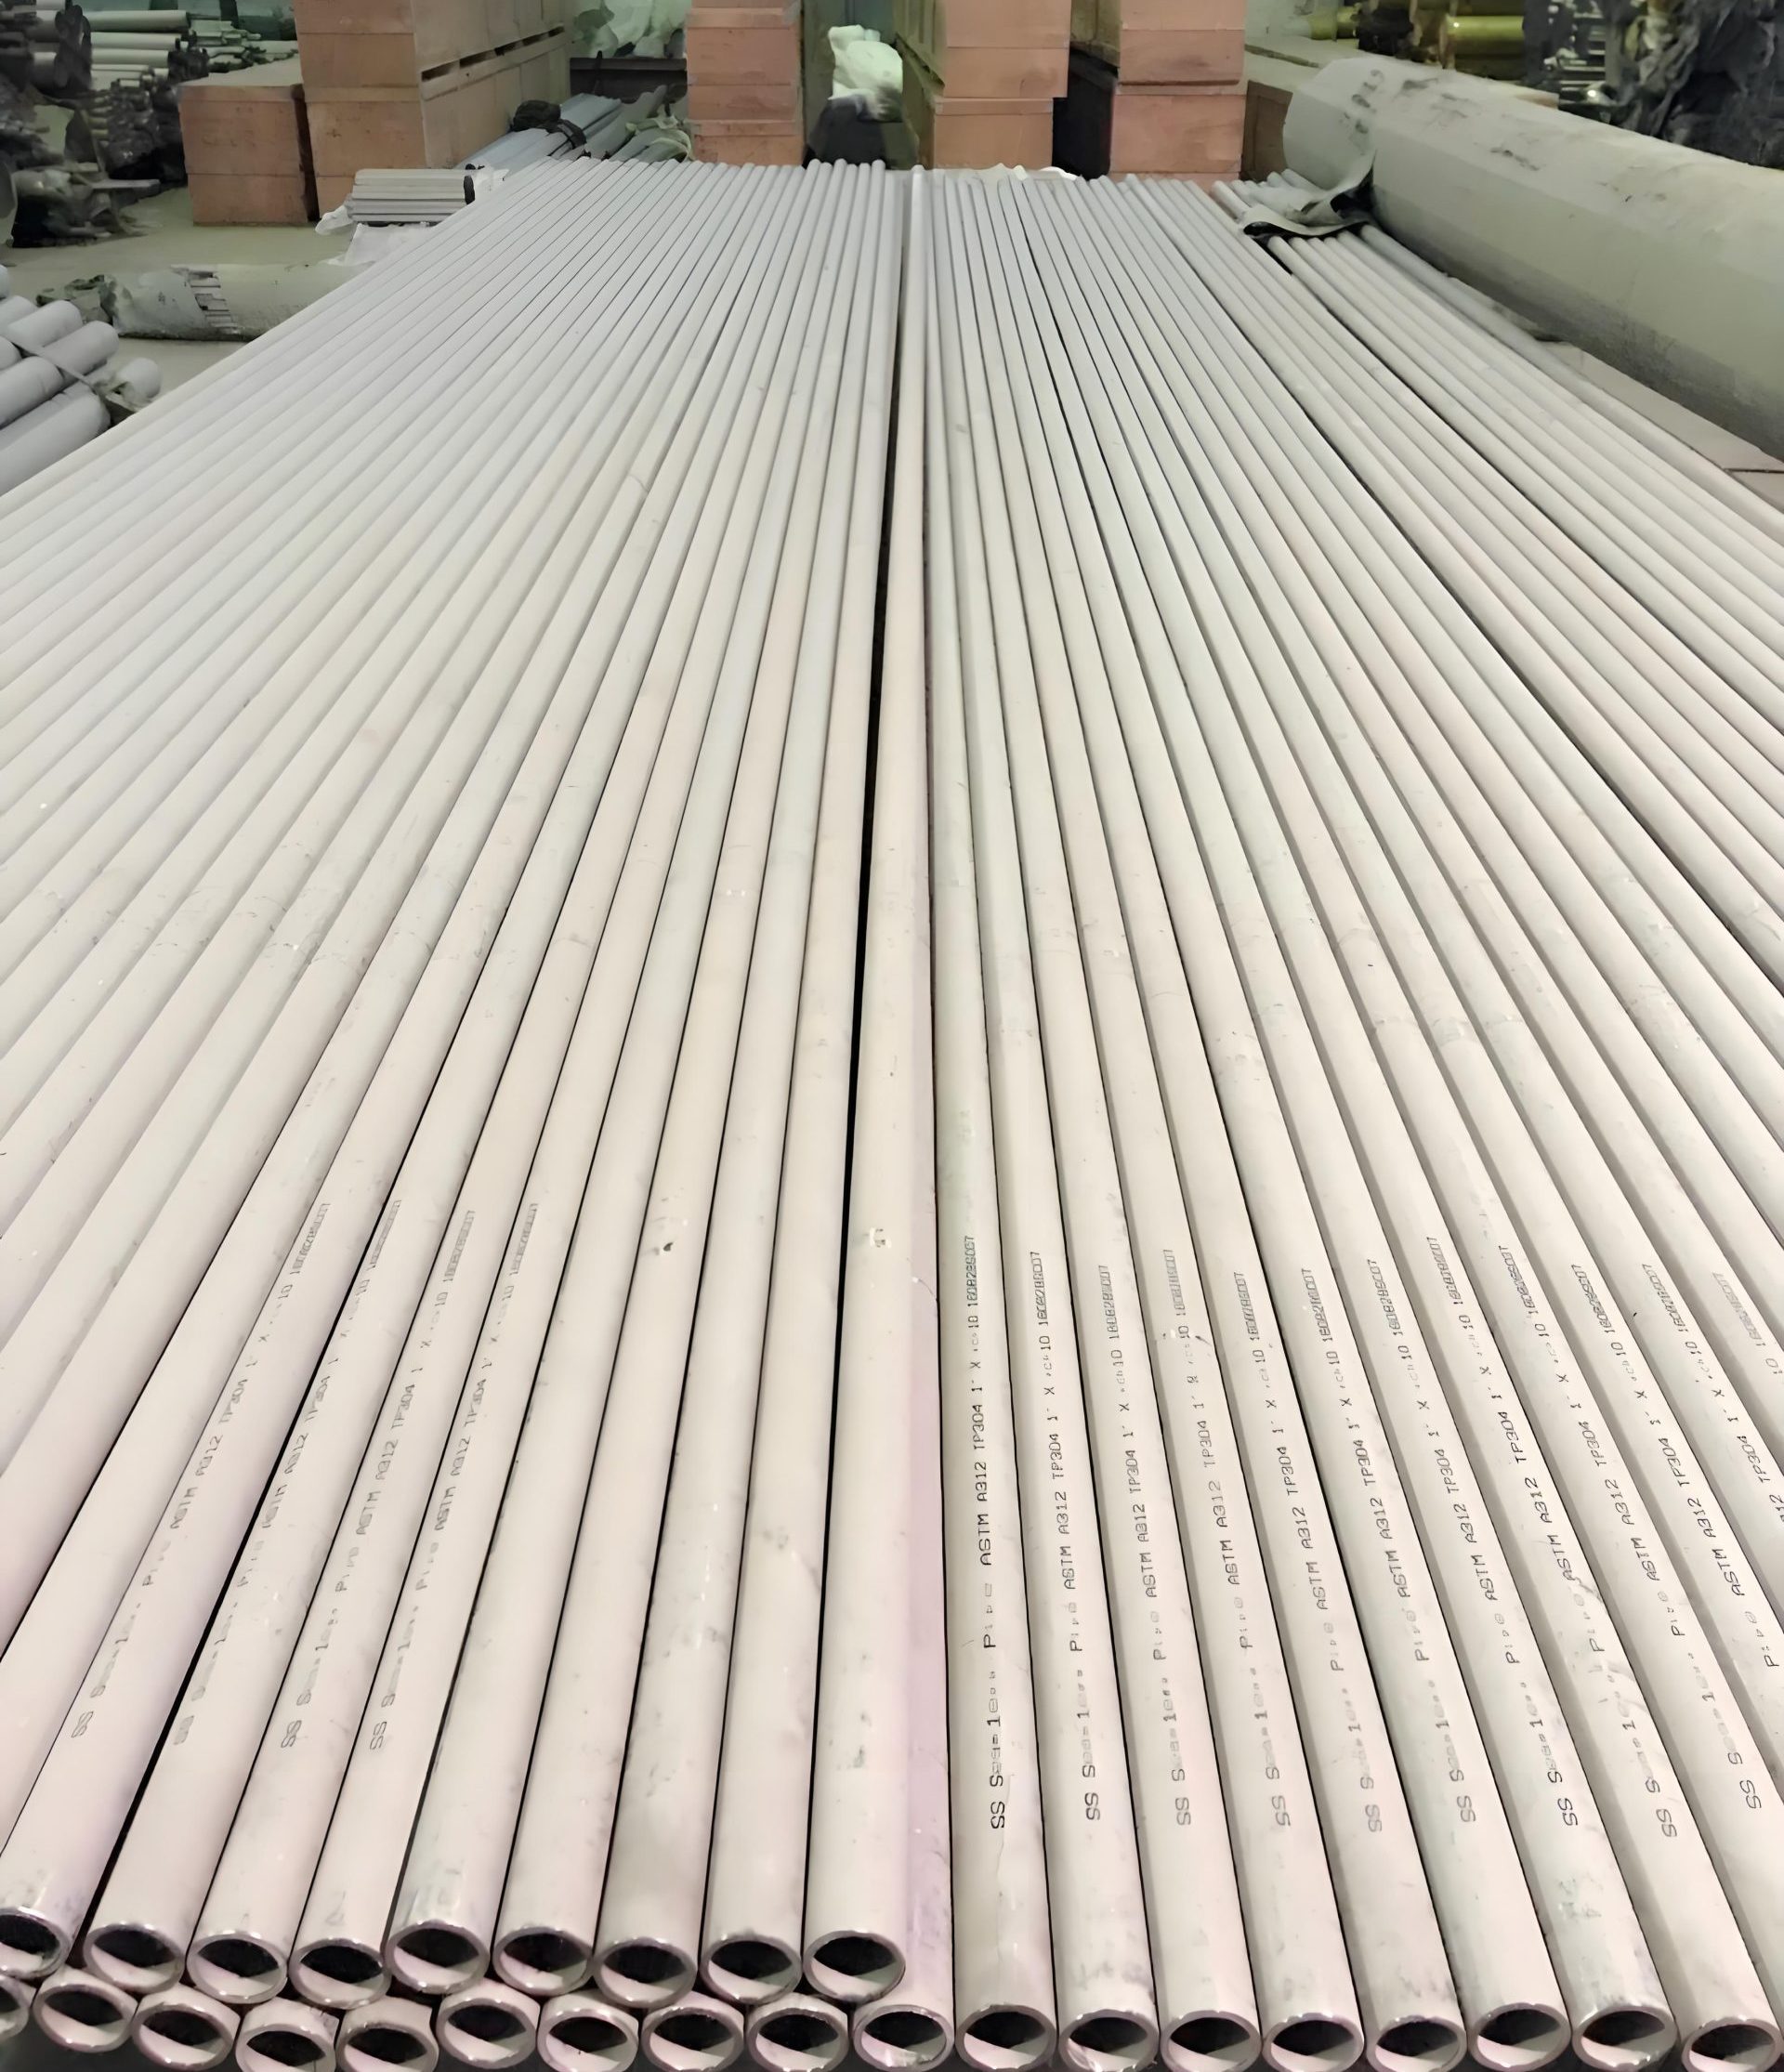
The predominant problem in welding X80 and above steels is guaranteeing that the fracture sturdiness of the weld metallic (WM) and HAZ suits or exceeds that of the base metallic (BM). Fracture toughness, quantified by means of metrics consisting of Charpy V-notch (CVN) effect energy and crack tip starting displacement (CTOD), is essential for fighting brittle failure, relatively in low-temperature environments or lower than dynamic loading like seismic hobbies or floor shifts. For illustration, API 5L requires minimal CVN energies of fifty-a hundred J at -20°C for X80 welds, depending on mission standards, at the same time CTOD values need to exceed zero.10 mm at the minimum design temperature to preclude pop-in cracks or cleavage fracture.
Key challenges include the formation of brittle microstructures within the HAZ, which includes martensite-austenite (M-A) materials or coarse-grained bainite, which act as crack initiation web sites. Additionally, oxygen pickup for the duration of welding introduces inclusions which can degrade durability with the aid of promoting cleavage or void coalescence. Optimizing weld materials components—somewhat achieving low oxygen content Shop Now material—and controlling welding heat enter are pivotal methods to mitigate these matters. Low oxygen degrees refine the microstructure by using minimizing oxide inclusions, at the same time genuine heat enter control impacts cooling premiums, grain dimension, and segment transformations. This paper explores those optimizations in aspect, drawing on experimental knowledge and marketplace practices to present actionable insights for reaching BM-similar or top of the line longevity in X80 and increased-grade welds.
Optimizing Weld Material Formulation: Emphasis on Low Oxygen Content
Weld material formulation plays a vital position in picking the mechanical houses of the WM, exceptionally its resistance to brittle fracture. For X80 and X100 pipeline steels, consumables would have to be selected or designed to overmatch the BM's yield energy (repeatedly 5-15% higher) while putting forward top sturdiness. Common procedures encompass gas metallic arc welding (GMAW), submerged arc welding (SAW), and flux-cored arc welding (FCAW), where the filler metallic chemistry rapidly influences oxygen incorporation.
Oxygen content in the weld steel, frequently from protective gasoline dissociation or flux decomposition, is a relevant parameter. At ranges above two hundred-three hundred ppm, oxygen varieties oxide inclusions (e.g., MnO, SiO2) that act as fracture nucleation websites, cutting CVN energies and CTOD values through facilitating dimple refinement or cleavage initiation. In excessive-force welds with martensitic microstructures, oxygen phases as low as one hundred forty ppm can shift the fracture mode from ductile to brittle, with upper shelf CVN energies losing noticeably. Conversely, ultra-low oxygen (underneath 50 ppm) promotes a cleanser microstructure ruled by way of acicular ferrite or quality bainite, modifying longevity devoid of compromising strength.
To succeed in low oxygen, sturdy wires are liked over metallic-cored or flux-cored variations, because the latter can introduce 50-a hundred ppm more oxygen by means of surface oxides or flux reactions. For example, in GMAW of X80, solid wires like ER100S-1 in achieving oxygen tiers of 20-25 ppm underneath argon-wealthy shielding (e.g., 82% Ar-18% CO2), yielding CVN values of 107 J at -60°C, compared to 41-sixty one J for metal-cored wires at 53 ppm oxygen. Optimization approaches embody due to deoxidizers like magnesium (Mg) or aluminum (Al) within the wire, which may scale back oxygen to 7-20 ppm in flux-cored wires, asserting fracture appearance transition temperatures (FATT) beneath -50°C even at higher strengths (360-430 HV).
Alloying facets extra refine the formulas. Manganese (Mn) at 1.4-1.6 wt% within the WM retards grain boundary ferrite formation and promotes acicular ferrite nucleation, boosting CVN longevity via 20-30%. Nickel (Ni) additions (zero.nine-1.3 wt%) atone for oxygen-prompted longevity loss in metallic-cored wires, stabilizing low-temperature bainite and achieving CTOD values of zero.14-zero.forty two mm at -10°C for X100 welds. Molybdenum (Mo) at 0.3-zero.five wt% enhances hardenability, when titanium (Ti) and boron (B) (optimized at 0.01-0.02 wt% Ti based on nitrogen stages) pin grain boundaries, cutting earlier austenite grain measurement (PAGS) and M-A formation. Cerium (Ce) additions (50-a hundred ppm) offer a unique system by way of converting Al2O3 inclusions to finer CeAlO3 dispersions, refining grain sizes and growing CVN from seventy three J to 123 J whilst elevating yield potential from 584 MPa to 629 MPa.
In perform, neural community items are hired to are expecting most advantageous chemistries, balancing oxygen, nitrogen, and alloying for X100 consumables like 1.0Ni-zero.3Mo wires, ensuring overmatching yield strengths of 838-909 MPa with CVN >249 J at -20°C. For area welding, self-shielded FCAW electrodes (e.g., E91T8-G) with Ni and coffee hydrogen (<4 ml/100g) minimize oxygen pickup, achieving HAZ CTOD >0.thirteen mm. These formulations be sure that WM longevity surpasses BM phases, with dispersion in CTOD values minimized to <0.1 mm variation.<p>
Optimizing Welding Heat Input: Microstructural Control for Enhanced ToughnessWelding heat input, defined as (voltage × current × 60) / (travel speed × 1000) in kJ/mm, profoundly affects cooling rates (t8/5, time from 800°C to 500°C) and thus the HAZ and WM microstructures. For X80 and higher steels, excessive heat input (>1.five kJ/mm) widens the HAZ (up to 2-3 mm), coarsens grains (PAGS >40 μm), and promotes upper bainite or M-A islands, which limit durability by means of growing native brittle zones (LBZs). Lower inputs (zero.three-zero.8 kJ/mm) speed up cooling (>15°C/s), favoring wonderful-grained minimize bainite or acicular ferrite, with end-cooling temperatures (FCT) round four hundred-500°C optimizing part steadiness.In the HAZ, thermal cycles result in regions like coarse-grained HAZ (CGHAZ, >1100°C), in which grain enlargement is maximum reported. High warmth inputs (1.four kJ/mm) yield CGHAZ widths of 1-1.5 mm with PAGS up to 50 μm, most well known to M-A extent fractions of five-10% and CTOD values as low as 0.forty seven mm at -10°C as a result of cleavage along grain boundaries. Multi-go welding exacerbates this through intercritically reheated CGHAZ (IRCGHAZ), forming necklace-category M-A (3-five μm) that initiates cracks, dropping CVN to <50 J at -30°C. Conversely, low warmth inputs (0.sixty five kJ/mm) restriction PAGS to fifteen μm, minimize M-A to blocky morphologies (<2 μm), and raise CTOD to 0.70 mm through deviating cracks into the ductile BM.</p>
For the WM, heat enter influences ferrite nucleation. At zero.32-0.fifty nine kJ/mm in tandem GMAW for X100, acicular ferrite dominates, yielding CVN of 89-255 J from -60°C to -20°C and CTOD >0.10 mm, meeting API minima. Preheat (50-100°C) and interpass temperatures (a hundred-a hundred and fifty°C) are needed to regulate hydrogen diffusion and hinder cracking, with induction heating making sure uniform application.Optimization consists of process qualification consistent with API 1104, targeting t8/5 of 5-10 s for X80, completed due to pulsed GMAW or regulated metallic deposition (RMD) for root passes, which cut down heat input via 20-30% whereas making improvements to bead profile. In slender-groove joints, higher go back and forth speeds (6-8 mm/s) diminish input to zero.34 kJ/mm, expanding productivity and tensile energy without durability loss. For girth welds, vertical-down FCAW at 1.4 kJ/mm requires Nb/Ti microalloying to restrict grain enlargement, guaranteeing HAZ CVN >one hundred J at -40°C.Data from simulated thermal cycles make certain that FCT underneath the bainite end temperature (three hundred°C) boosts energy but hazards durability; subsequently, hybrid cooling (extended publish-weld) is suggested for X100, reaching vTrs (CVN transition) below -eighty°C.
Integrated Approaches and Case Studies
Combining low-oxygen formulations with managed heat input yields synergistic blessings. In a PHMSA-funded learn about on X100, dual-tandem GMAW with 1.0Ni-zero.3Mo wires (20 ppm O) at 0.43 kJ/mm produced welds with YS overmatch of 10%, CVN 255 J at fusion line (-20°C), and CTOD zero.sixty seven mm, exceeding BM by way of 15%. Another case for X80 girth welds used RMD root passes (low H2, 25 ppm O) followed by using pulsed fill at 0.7 kJ/mm, reaching uniform HAZ longevity (CVN >one hundred fifty J at -50°C) devoid of put up-weld warmth medication.Post-weld solutions like stress alleviation (600°C) can refine M-A but may not invariably give a boost to CTOD in X80, emphasizing proactive optimization.ConclusionOptimizing weld drapery for extremely-low oxygen (<50 ppm) by the use of deoxidized wires and alloying (Ni, Mn, Ce) , coupled with warmness inputs of zero.3-zero.8 kJ/mm for turbo cooling, guarantees X80+ welds reach greatest fracture sturdiness. These systems, established by in depth trying out, safeguard pipeline reliability.<p>